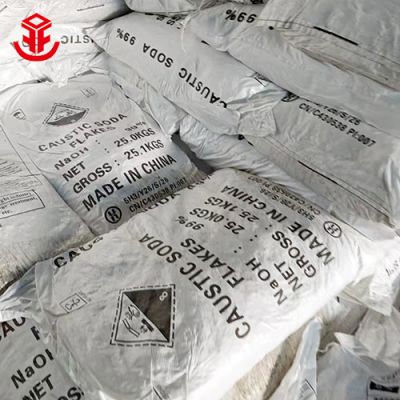
In modern chemical production and manufacturing, maintaining consistency in raw material quality is critical to process reliability and operation safety. Our NaOH 25kg industrial grade product is manufactured under strict quality standards, offering high reactivity, excellent purity, and robust multi-layer packaging tailored for global shipping and long-term warehousing.
Purity Level: High assay concentration of 99% min, with trace impurities such as sodium carbonate and heavy metals kept well below standard industrial thresholds.
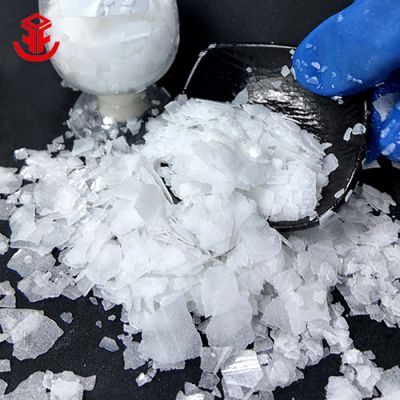
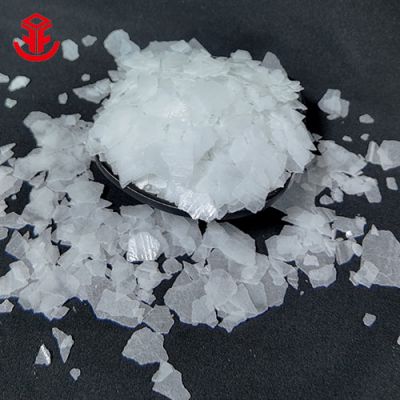
Physical Form: White crystalline flakes that dissolve rapidly in water, initiating an exothermic reaction and forming a strongly alkaline solution.
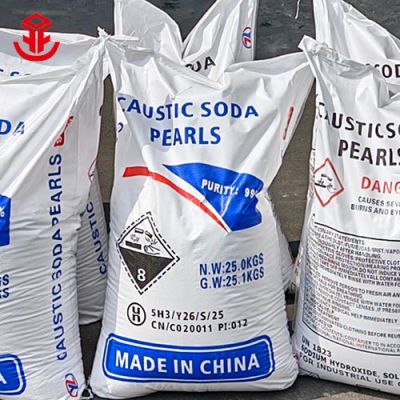
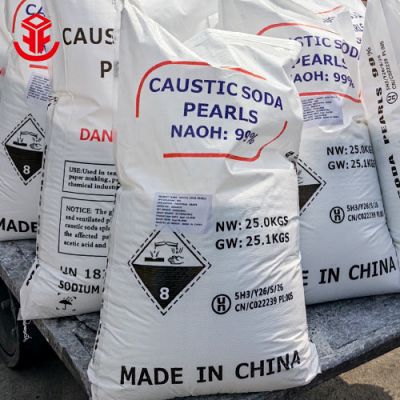
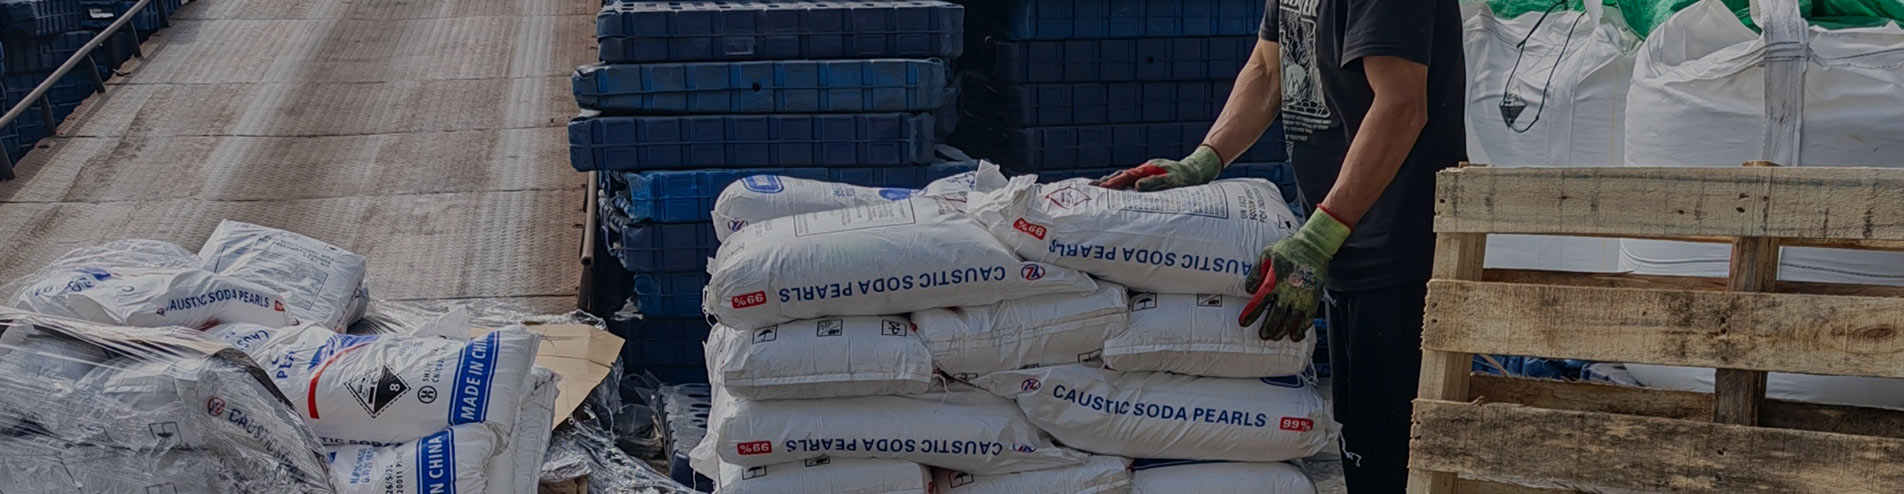
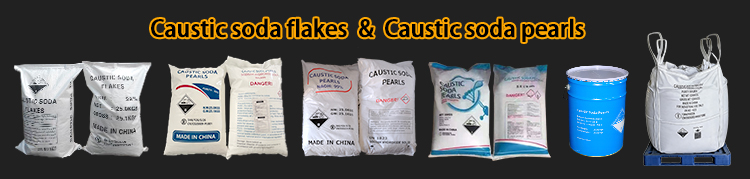
Packaging Specification: Standardized 25kg bags built with an internal heavy-duty polyethylene (PE) liner and a tear-resistant woven exterior to withstand humidity, stacking, and long-distance maritime transport.
In industrial effluent processing facilities, NaOH 25kg supplies serve as an essential agent for adjusting pH balances. The strong alkaline property rapidly neutralizes acidic wastewater streams, facilitates heavy metal precipitation, and optimizes flocculation efficiency in compliance with environmental discharge regulations.
The textile sector utilizes this compound for desizing, scouring, and mercerizing cotton fibers to enhance dye absorption, fabric strength, and surface luster. In pulping operations, it acts as a key cooking agent to break down lignin and separate cellulose fibers, ensuring efficient paper pulp preparation.
As a foundational alkali in chemical synthesis, it reacts with plant fats and animal lipids during the saponification process to produce solid soap bases and surfactants. Additionally, it serves as a core builder in heavy-duty commercial cleaners, degreasers, and automated CIP (Clean-in-Place) equipment washing protocols.
To maintain product efficiency and prevent atmospheric moisture absorption:
Dry Storage Environment: Store in a cool, well-ventilated warehouse away from direct sunlight and humidity.
Incompatibility Management: Keep segregated from acids, organic peroxides, flammable substances, and reactive metals like aluminum or zinc.
Personal Protective Equipment (PPE): Handlers must wear chemical-resistant gloves, protective goggles, and full-body apron protection to avoid contact with skin and eyes.
 Fangyuan(Tianjin) Chemical Co.,ltd...[ read more ]


Contact Person:Alice Wang
Tel:86-18622179529
Mobile Phone:86-18622179529
WhatsApp:86-18622179529
E-mail:admin@fangyuan-chem.com
Add:Room 908, Yinzuo Building, No. 35, Second Avenue, Tianjin Economic and Technological Development Area