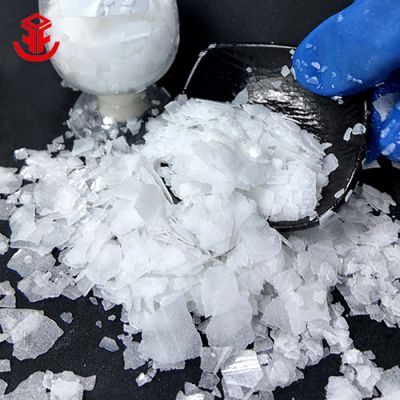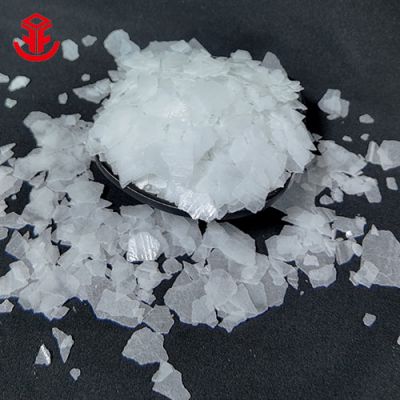
In today's global food and beverage manufacturing ecosystem, absolute quality control, regulatory adherence, and strict sanitary standards form the foundation of brand trust. Processing chemicals used across production lines must meet stringent purity thresholds to ensure consumer safety while optimizing operational yield. Premium food grade caustic soda serves as a vital processing aid across large-scale kitchens, dairy plants, beverage bottling lines, and agricultural processing facilities.
Formulated to align seamlessly with global food chemical standards—such as the European Union E524 regulations and Codex alimentarius criteria—this high-potency alkaline agent delivers dependable performance for pH adjustment, chemical peeling, and intensive industrial sanitization.
Cleanliness is non-negotiable in food production. In modern breweries, dairy operations, and juice packaging lines, organic residues such as milkstone, fats, complex proteins, and sugars accumulate rapidly inside heat exchangers, pipelines, and holding tanks. Food grade caustic soda functions as a primary active sanitizing agent. It rapidly breaks down fatty acids through saponification and hydrolyzes tough protein chains, removing stubborn baked-on deposits without requiring time-consuming manual equipment disassembly.
Commercial beverage operations that utilize reusable glass packaging require extreme cleanliness before refilling. High-temperature alkaline bath solutions utilizing food grade caustic soda efficiently dissolve adhesives, strip legacy paper labels, neutralize micro-contaminants, and remove organic surface films. This processing guarantees brilliant clarity and biologically safe containers ready for high-speed automatic filling lines.
For agricultural processing plants, maintaining product integrity while maximizing yield is crucial. Diluted, controlled baths of high-purity caustic soda are widely used for the chemical peeling of tomatoes, potatoes, carrots, peaches, and citrus segments. The solution gently loosens the outer peel without damaging the underlying fruit flesh, resulting in higher usable yields, reduced waste, and superior visual appearance in canned or frozen consumer goods.
Bakery Products: Immersing pretzel dough in a mild alkaline solution prior to baking catalyzes an accelerated Maillard reaction, yielding the characteristic deep golden-brown crust, shiny finish, and iconic flavor signature.
Olive Processing: Controlled alkaline baths soften bitter compounds like oleuropein in freshly harvested green olives, accelerating the curing timeline while preserving desirable crunch.
Cocoa Alkalization: Treating cocoa mass or powder adjusts natural acidity, darkens color intensity, and improves dispersibility for instant chocolate drinks and premium confectionery.
Our food grade caustic soda stands out through strict raw material selection and engineered physical consistency. Certified fully compliant with E524 and FCC criteria, every batch is guaranteed safe for direct and indirect food processing. Featuring an exceptional purity profile that typically exceeds 99%, the material maintains ultra-low trace heavy metals, effectively eliminating the risk of batch contamination or off-flavors.
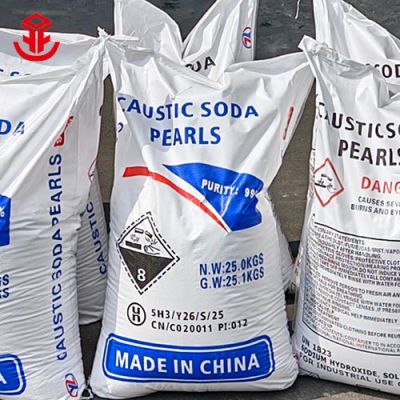
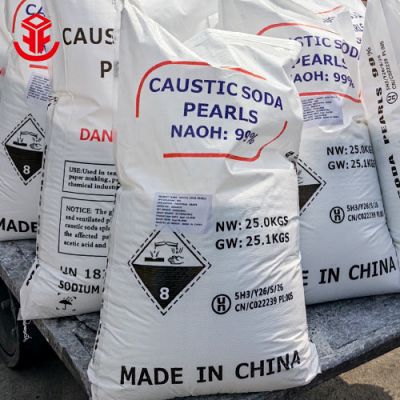
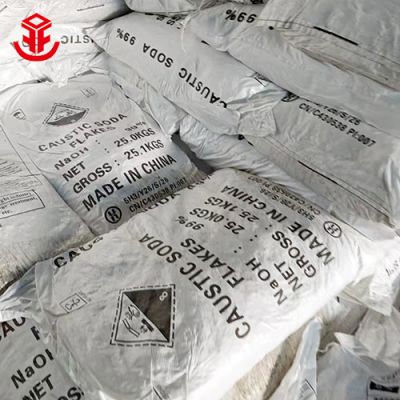
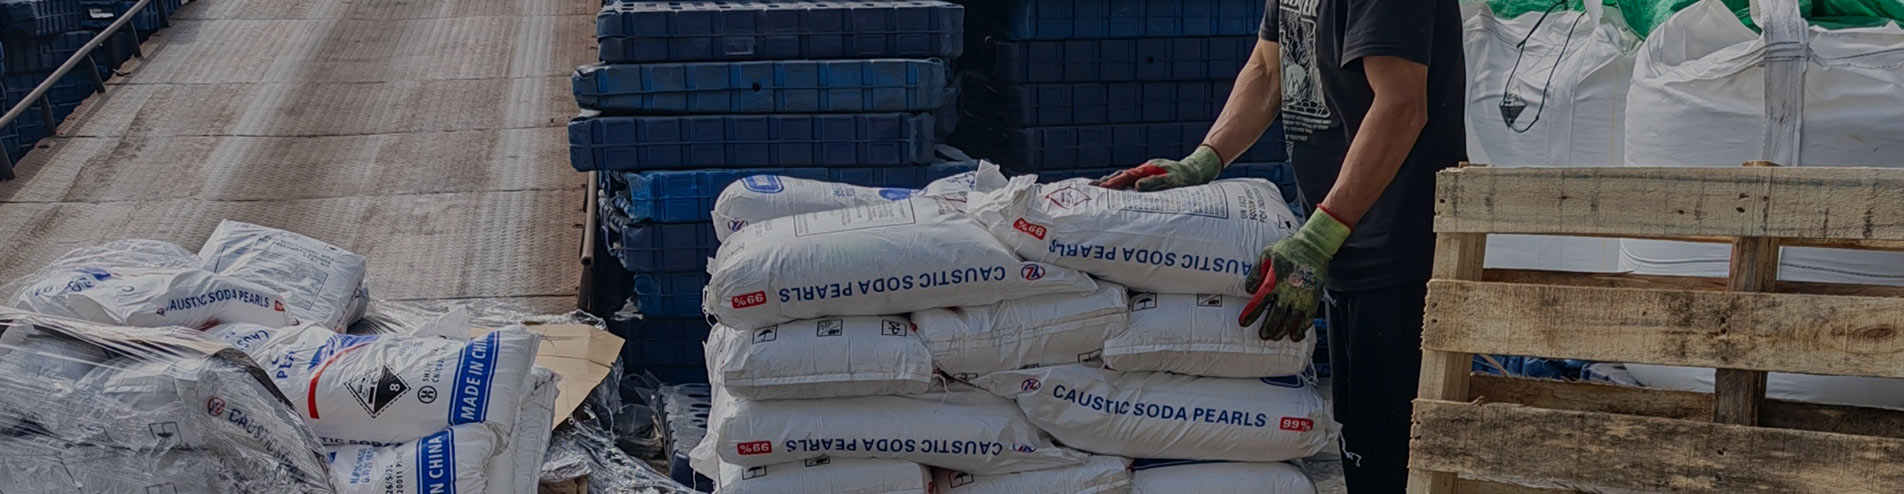
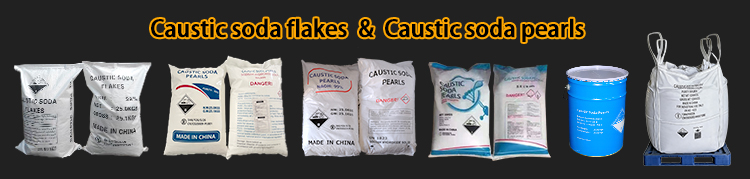
In terms of physical performance, the product offers rapid, predictable dissolution dynamics whether ordered in high-density micro-pearls or uniform flakes. This ensures seamless automatic dosing and prevents hot-spot thermal concentration spikes during initial solution preparation. Furthermore, the material is packaged in moisture-resistant, heavy-duty multi-ply packaging that prevents clumping during international transit and extended warehouse storage, ensuring hassle-free manual or pneumatic handling at your production site.
Establishing resilient cross-border supply chains requires complete transparency and verified quality controls. Every shipment of our food grade caustic soda undergoes exhaustive analytical testing in accredited laboratories before dispatch.
Certificate of Analysis (CoA): Shipped alongside every container to confirm batch purity, exact physical form, and compliance with heavy metal limits.
Regulatory Rigor: Produced in facilities adhering strictly to Hazard Analysis Critical Control Point (HACCP) protocols and ISO manufacturing standards.
End-to-End Traceability: Complete lot tracking codes ensure clear visibility from primary material processing down to plant-level delivery.
Because high-strength alkaline chemicals possess reactive characteristics, facility personnel must implement proper handling procedures and utilize standard protective gear. Products should be stored in unopened original packaging within cool, dry, and well-ventilated dedicated warehouse zones away from incompatible acids. Containers must remain tightly sealed after open dosing steps to avoid moisture uptake and atmospheric carbonation.
Elevate your processing efficiency and protect your finished product standard with a dependable global chemical supplier. Contact our technical engineering team today to request Safety Data Sheets (SDS), Technical Data Sheets (TDS), or custom commercial price quotes.
 Fangyuan(Tianjin) Chemical Co.,ltd...[ read more ]


Contact Person:Alice Wang
Tel:86-18622179529
Mobile Phone:86-18622179529
WhatsApp:86-18622179529
E-mail:admin@fangyuan-chem.com
Add:Room 908, Yinzuo Building, No. 35, Second Avenue, Tianjin Economic and Technological Development Area