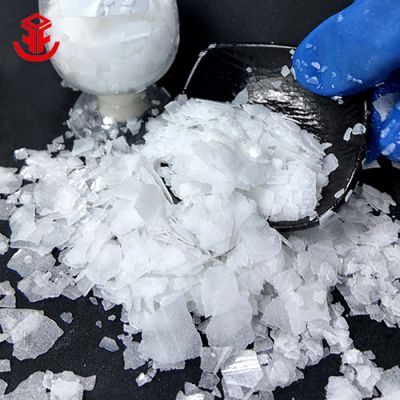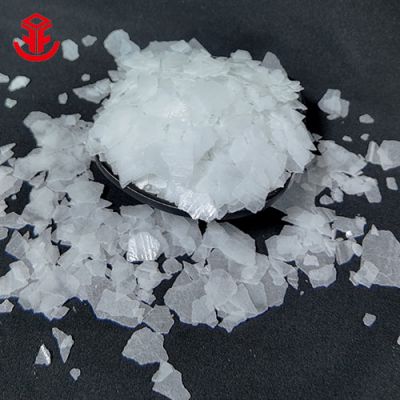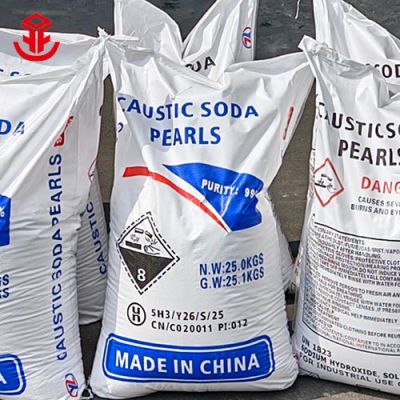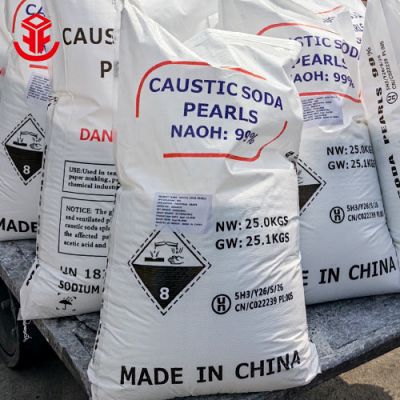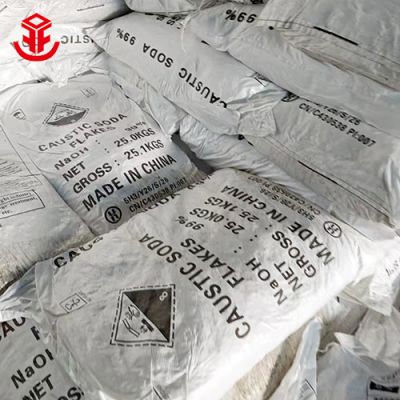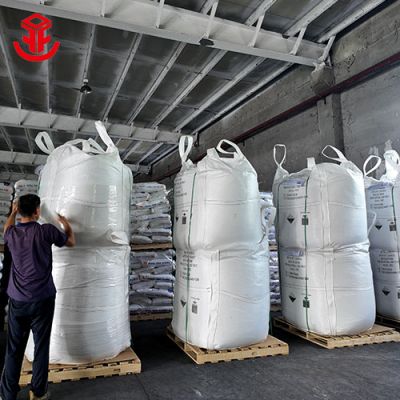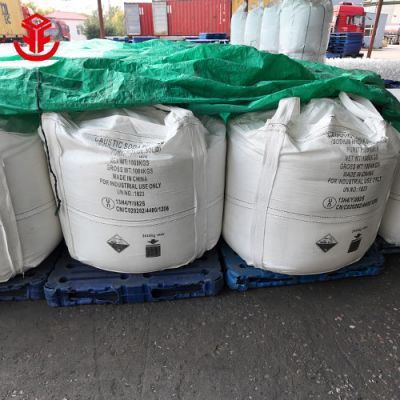
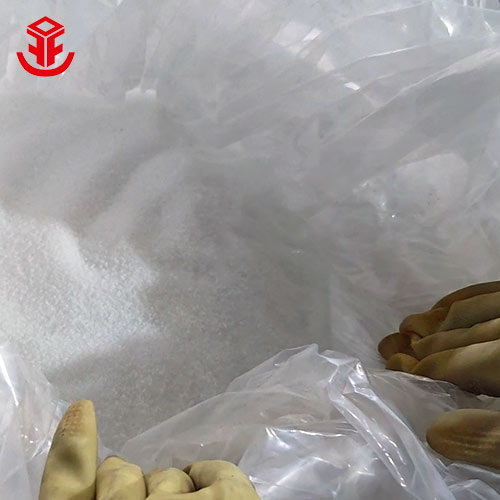
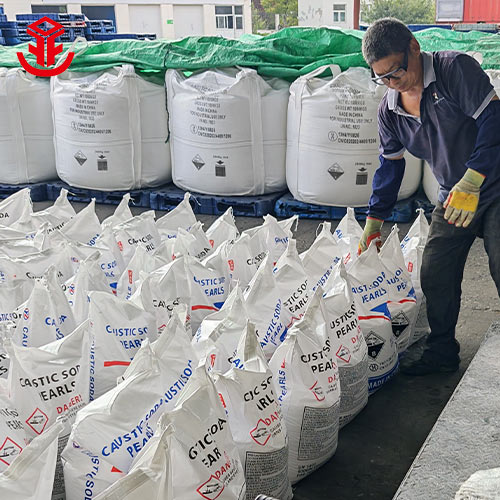
Our Caustic Soda Jumbo units offer an optimized, cost-effective raw material solution for large-volume industrial operators. Processed to exacting quality standards, this strong alkali chemical delivers consistent reactivity for pulp and paper processing, textile processing, alumina extraction, soap synthesis, and heavy wastewater neutralisation.
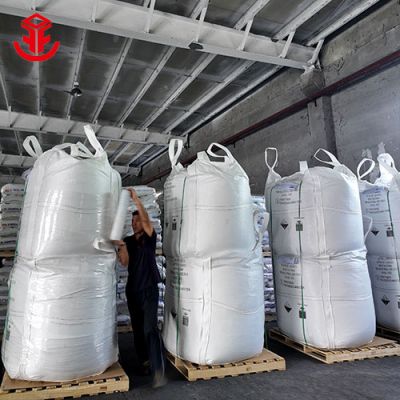
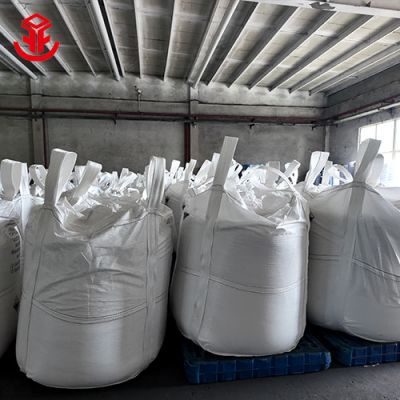
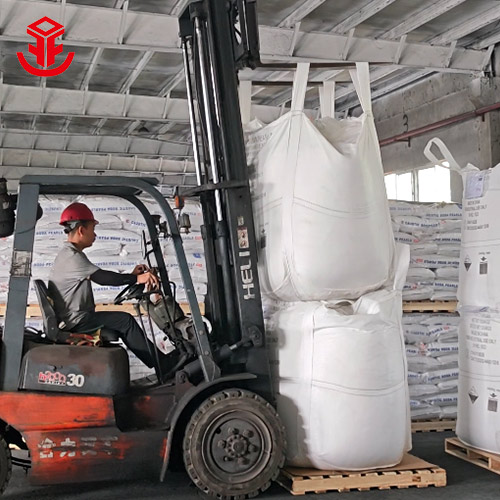
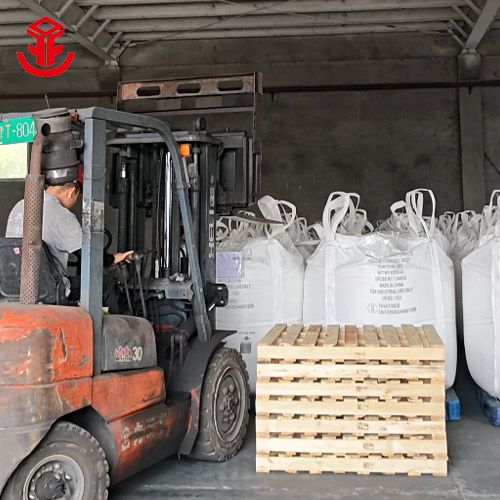
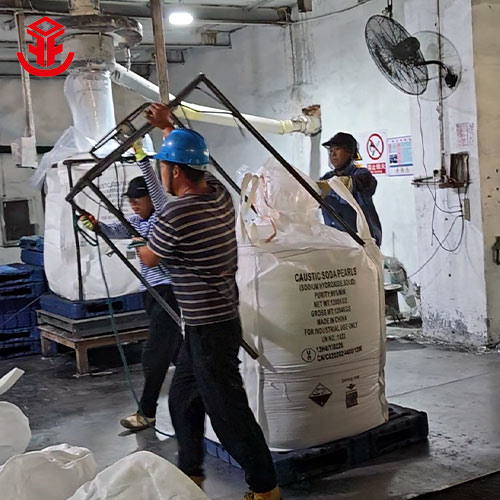
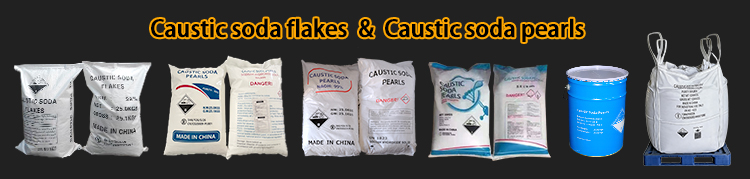
Each Jumbo packaging system contains 1,000 kg of high-concentration material housed within multi-layer, moisture-resistant polypropylene packaging. Engineered with robust lifting loops and UV-stabilized woven structures, our jumbo sacks prevent environmental contamination and moisture absorption during long-distance maritime transit. Partnering with us ensures a steady bulk supply line, competitive factory-direct pricing, and compliance with global safety transport guidelines. Streamline your bulk chemical logistics and optimize your plant operations with our dependable industrial supply.
In modern heavy industries, securing stable, high-grade alkaline raw materials is crucial for maintaining production consistency and thermal-chemical control. Our Caustic Soda Jumbo packaging solution provides heavy chemical consumers with seamless integration into continuous production systems. Manufactured under stringent quality assurance protocols, this white, highly deliquescent alkaline solid is essential for saponification, neutralization, organic synthesis, and pH regulation across diverse sectors.
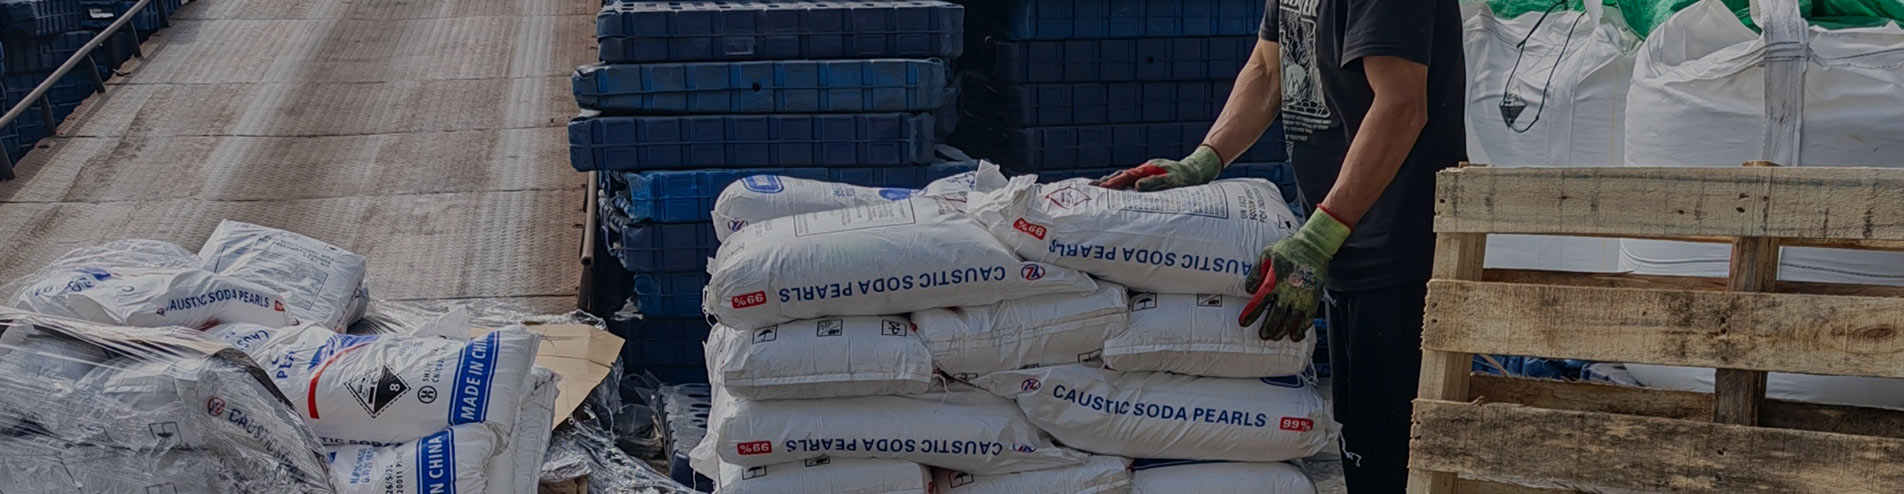
By ordering in jumbo quantities, processing facilities significantly reduce handling labor, warehouse footprints, and packaging waste compared to standard 25kg bags. Whether applied in water treatment infrastructure or primary metal refining, this product delivers exceptional purity and rapid dissolution rates to keep your reaction vessels operating at peak efficiency.
Quality consistency is the backbone of successful chemical manufacturing. Our products are thoroughly monitored during crystallization, flake/pellet formulation, and bagging to ensure minimal moisture contamination and zero foreign matter.
Key technical advantages include:
High Reactivity: Exceptional concentration guarantees precise chemical dosing and fast reaction kinetics in aqueous solutions.
Low Impurity Levels: Negligible heavy metals and iron content safeguard your secondary catalysts and fine chemical products from contamination.
Anti-Caking Performance: Modern bagging technologies prevent humidity intake, keeping flakes and pearls free-flowing for easy automated discharge into hoppers.
Reinforced Packaging & Global Logistics
Transporting hazardous alkalis across international shipping routes demands zero compromise on package integrity. Our Jumbo units are specifically engineered to withstand harsh maritime environments, thermal shifts, and mechanical stress.
Heavy-Duty Construction: Outer bags are crafted from UV-stabilized woven polypropylene, reinforced with cross-corner cross-stitching to ensure zero seam failure during crane hoisting.
Hermetic Moisture Barrier: Each sack incorporates a thick internal polyethylene liner that isolates the chemical from atmospheric humidity, moisture ingress, and ambient gases.
Optimized Containerization: Sized precisely for standard ISO shipping containers, allowing maximum weight density per freight container and lowering your per-ton shipping cost.
Our bulk-packaged strong alkali serves as a core foundation for numerous essential global industries:
Pulp and Paper Manufacturing: Essential for digesting wood chips during the Kraft process, removing lignin, and bleaching pulp fibers.
Textile & Dyeing Industries: Used extensively for mercerizing cotton fabric, enhancing fiber dye absorbency, and refining raw synthetic materials.
Alumina & Metal Extraction: Acts as a vital reagent in digesting bauxite ore to extract pure alumina, a primary precursor to aluminum metal production.
Water Treatment & Environmental Protection: Neutralizes acidic industrial wastewater streams, removes toxic heavy metals via precipitation, and controls municipal water pH.
Soaps & Detergent Processing: Drives the saponification reaction that breaks down fats and triglycerides into soaps and high-grade surfactants.
Because bulk strong alkalis react vigorously with moisture, acidic substances, and active metals like aluminum or zinc, adhering to proper storage and safety protocols is necessary. Always store jumbo bags in a well-ventilated, moisture-free warehouse fitted with concrete flooring. Keep containers tightly closed when not in use. Handlers must utilize appropriate personal protective gear, including chemical-resistant suits, heavy-duty gloves, face shields, and safety goggles. Mechanical unloading systems should utilize broad webbing slings to ensure safe overhead lifting.
Why Choose Our Bulk Supply?
Partnering with an experienced bulk chemical exporter means reliability from factory loading to final delivery. We offer flexible manufacturing schedules, customized packaging logos, rigorous third-party batch inspections (such as SGS/Intertek), and dedicated maritime logistics support. Protect your supply chain from market shortages and price volatility by establishing a long-term supply agreement with us today.
 Fangyuan(Tianjin) Chemical Co.,ltd...[ read more ]


Contact Person:Alice Wang
Tel:86-18622179529
Mobile Phone:86-18622179529
WhatsApp:86-18622179529
E-mail:admin@fangyuan-chem.com
Add:Room 908, Yinzuo Building, No. 35, Second Avenue, Tianjin Economic and Technological Development Area