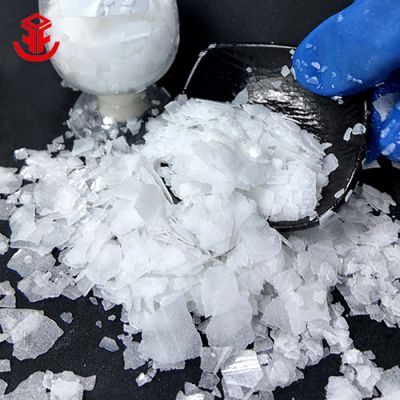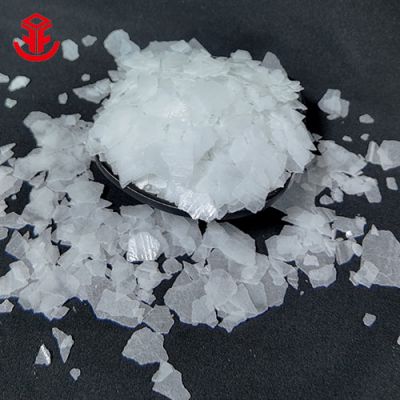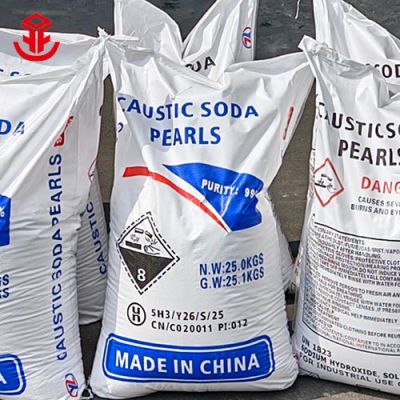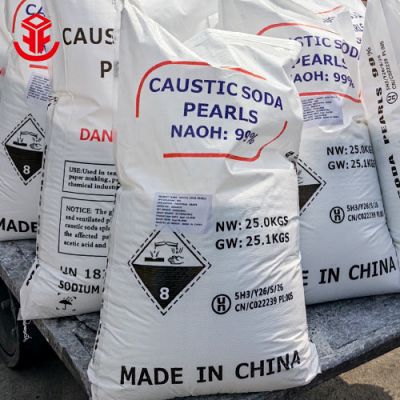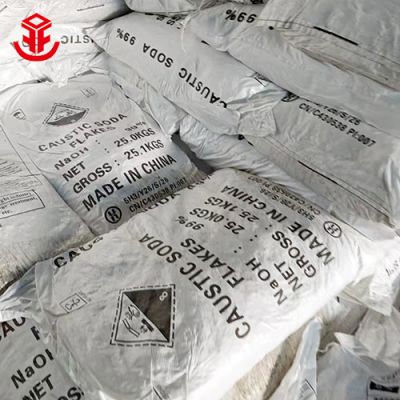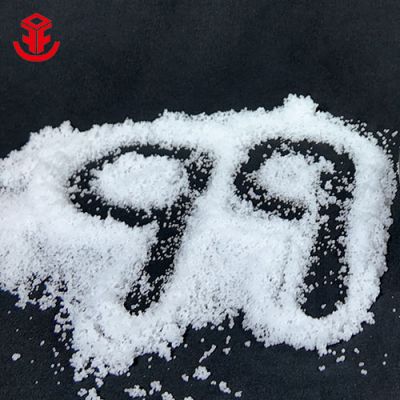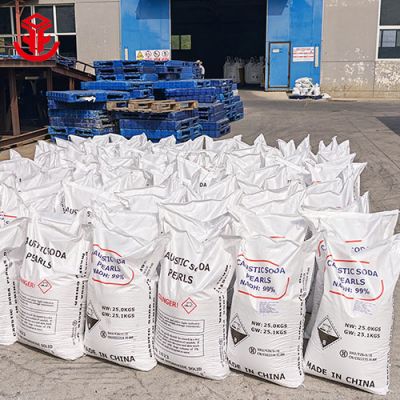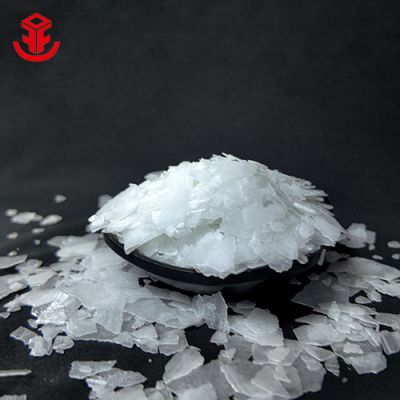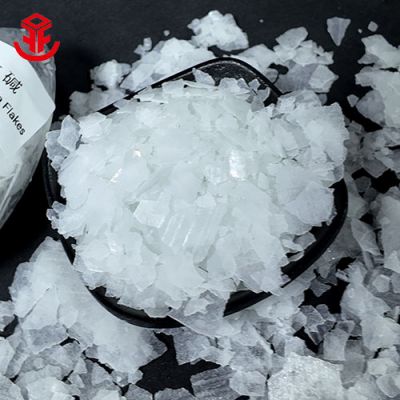
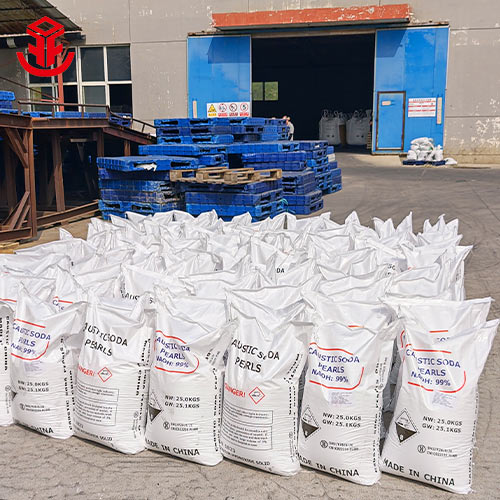
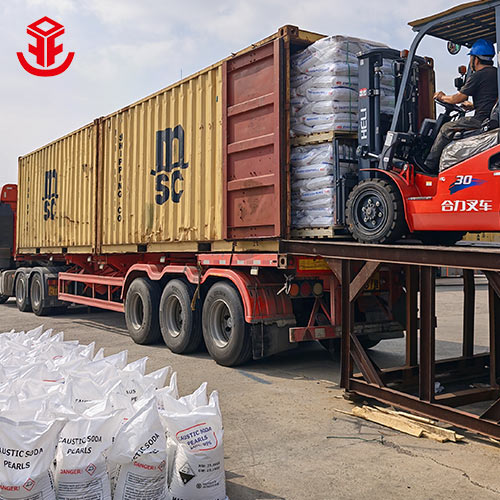
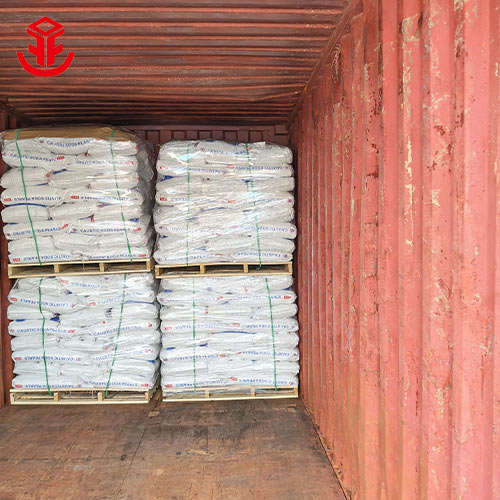
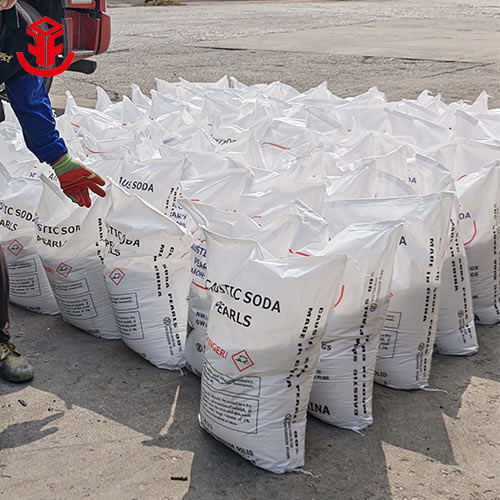
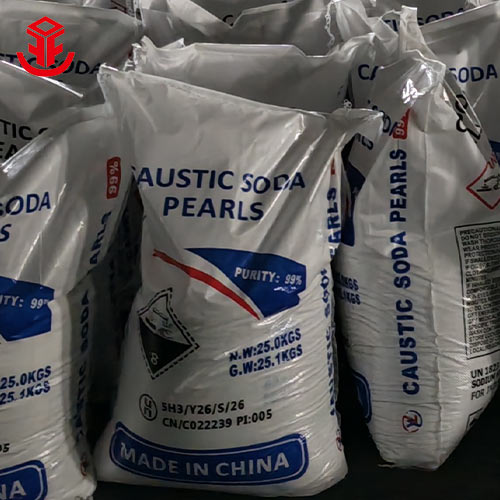
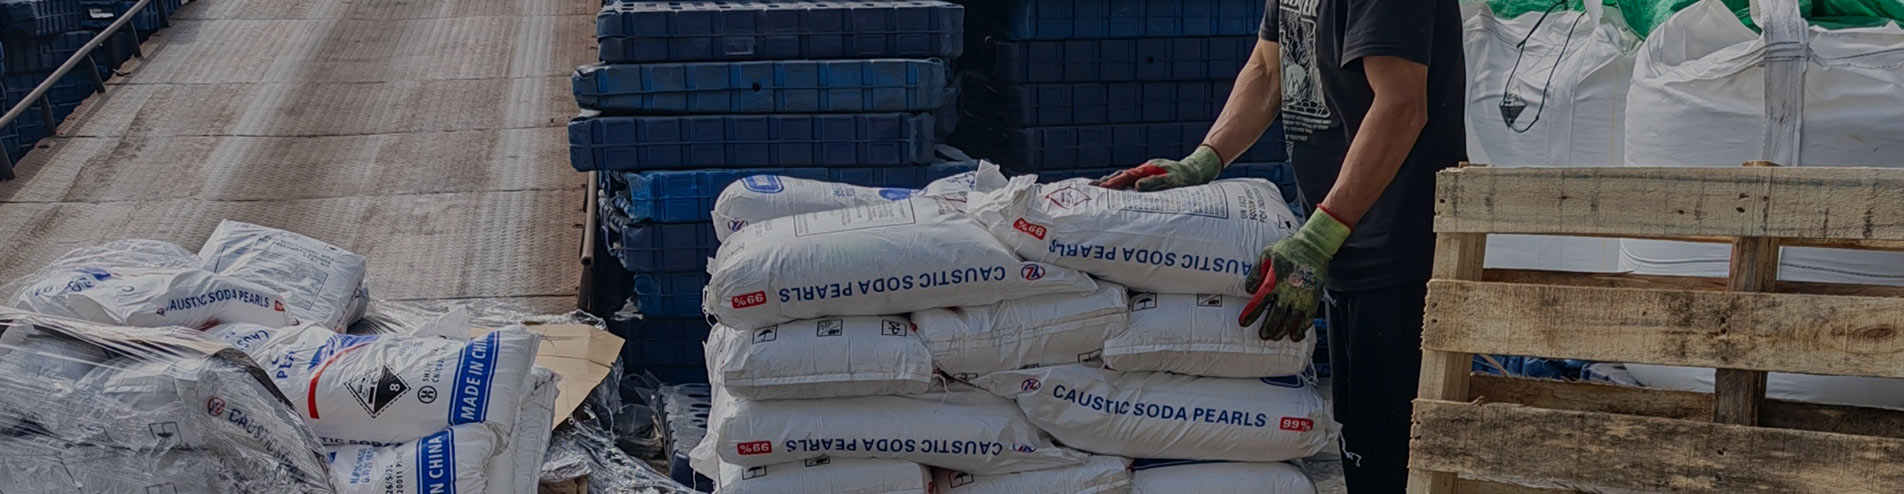
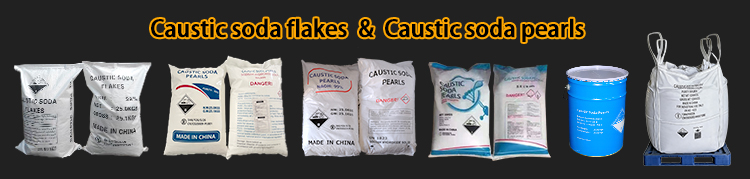
Our industrial grade caustic soda bag package provides an exceptionally safe and reliable solution for chemical transportation and processing. Each caustic soda bag is constructed from high-tensile poly-woven material reinforced with a thick inner polyethylene liner. This dual-layer design creates an impenetrable barrier against moisture, humidity, and external contaminants, ensuring that the 99% pure alkaline pearls remain completely free-flowing, dry, and active during long-distance transit. Engineered specifically for demanding industrial applications such as water treatment, soap manufacturing, textile processing, and chemical synthesis, this packaging guarantees zero degradation of product activity. By choosing our reinforced bags, global buyers minimize product loss, avoid chemical caking, and optimize warehouse stacking. The standardized 25kg bag size fits international pallet standards, facilitating efficient freight handling and automated plant operations worldwide.
Exceptional Packaging Standard for Maximum Safety
When dealing with strong alkaline chemicals, packaging integrity is as important as chemical purity itself. Every caustic soda bag engineered by our team utilizes a high-strength woven polypropylene outer jacket combined with a hermetically sealed inner PE liner. This dense, multi-layer construction effectively protects the contents from atmospheric moisture, ambient humidity, and chemical leeching. Moisture exposure causes alkaline compounds to cake or dissolve prematurely, which compromises material handling in processing plants. Our reinforced bags ensure that every shipment arrives in pristine, dry condition, preserving the full 99% active strength of the solid pearl formulation.
Tailored for Global Logistics and Freight Efficiency
International trade demands rigorous packaging performance. Our caustic soda bag units are specifically customized to endure the stresses of ocean shipping, multi-modal transport, and rugged port handling. The heavy-duty stitching and tear-resistant material structure resist accidental punctures, preventing expensive product leakage during palletizing or forklift handling. The standard 25kg volumetric sizing is carefully calibrated to optimize pallet utilization inside 20ft and 40ft ocean containers. By standardizing bulk shipments on sturdily stacked pallets, we help clients reduce freight overhead, increase safety during unloading, and maximize warehouse vertical storage capacities.
Diverse Industrial Applications
The contents within each caustic soda bag serve critical operational functions across dozens of heavy industries around the globe:
Water Treatment & Environmental Engineering: Used extensively for neutralizing acidic industrial wastewater, adjusting pH levels in municipal water systems, and removing heavy metal ions during water clarification processes.
Soap & Detergent Manufacturing: Acts as a fundamental reactant in saponification, turning fats and oils into high-quality commercial soaps, industrial cleansers, and heavy-duty degreasers.
Textile & Dyeing Industry: Essential for mercerizing cotton fabrics to increase tensile strength and dye receptivity, as well as scouring raw materials prior to processing.
Pulp & Paper Production: Serves in the Kraft pulping process to dissolve lignin from wood fibers, yielding strong bleached paper products.
Chemical Synthesis & Refining: Used as a basic alkaline feedstock for synthesizing organic and inorganic chemical derivatives, alumina refining, and equipment sanitation.
Quality Assurance and Safe Handling Practices
Safety and quality compliance drive our entire production chain. Every batch contained within our caustic soda bag inventory undergoes strict lab testing to guarantee high purity, low impurity levels, and uniform particle size. Clear, standardized hazard warnings, GHS pictograms, and multi-language handling instructions are printed directly on the exterior of each bag to ensure regulatory compliance and worker safety at destination facilities. For safe operational handling, operators should store bags in a cool, well-ventilated, dry warehouse away from acidic materials and flammable substances.
Why Choose Our Bagged Chemical Solutions?
Partnering with us guarantees direct access to dependable bulk supply, stable chemical specifications, and export-grade packaging built for harsh shipping environments. Whether you require containerized shipments or tailored pallet configurations, our flexible supply chain ensures timely delivery, helping keep your production lines running smoothly without disruption.
 Fangyuan(Tianjin) Chemical Co.,ltd...[ read more ]


Contact Person:Alice Wang
Tel:86-18622179529
Mobile Phone:86-18622179529
WhatsApp:86-18622179529
E-mail:admin@fangyuan-chem.com
Add:Room 908, Yinzuo Building, No. 35, Second Avenue, Tianjin Economic and Technological Development Area